High-performance tissue, kitchen roll, and napkin products engineered to rigorous international B2B quality standards.
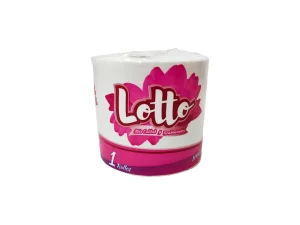
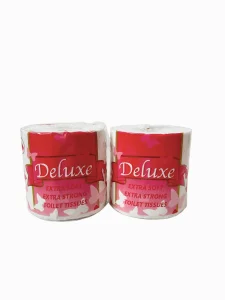
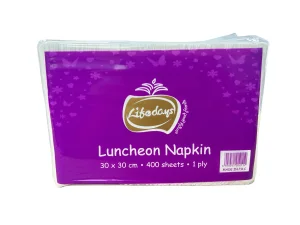
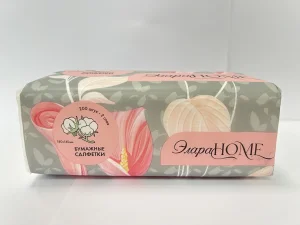
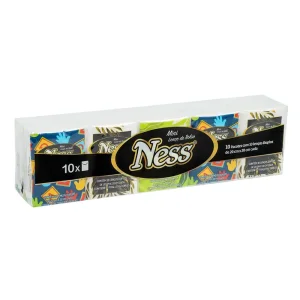
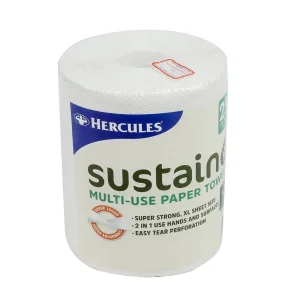
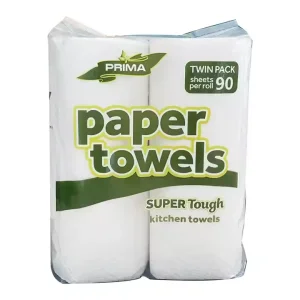
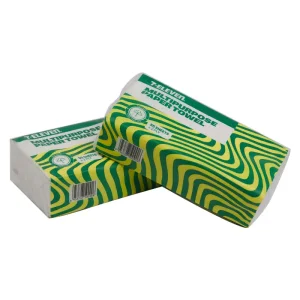
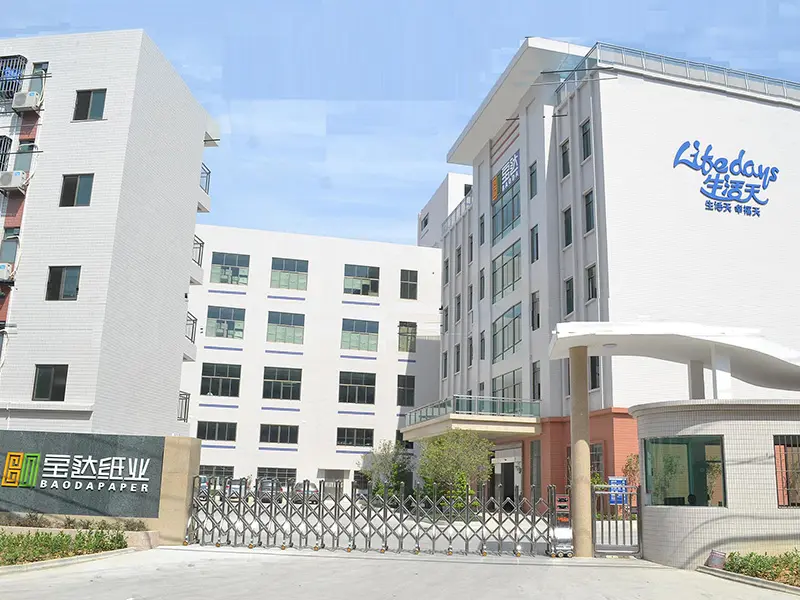
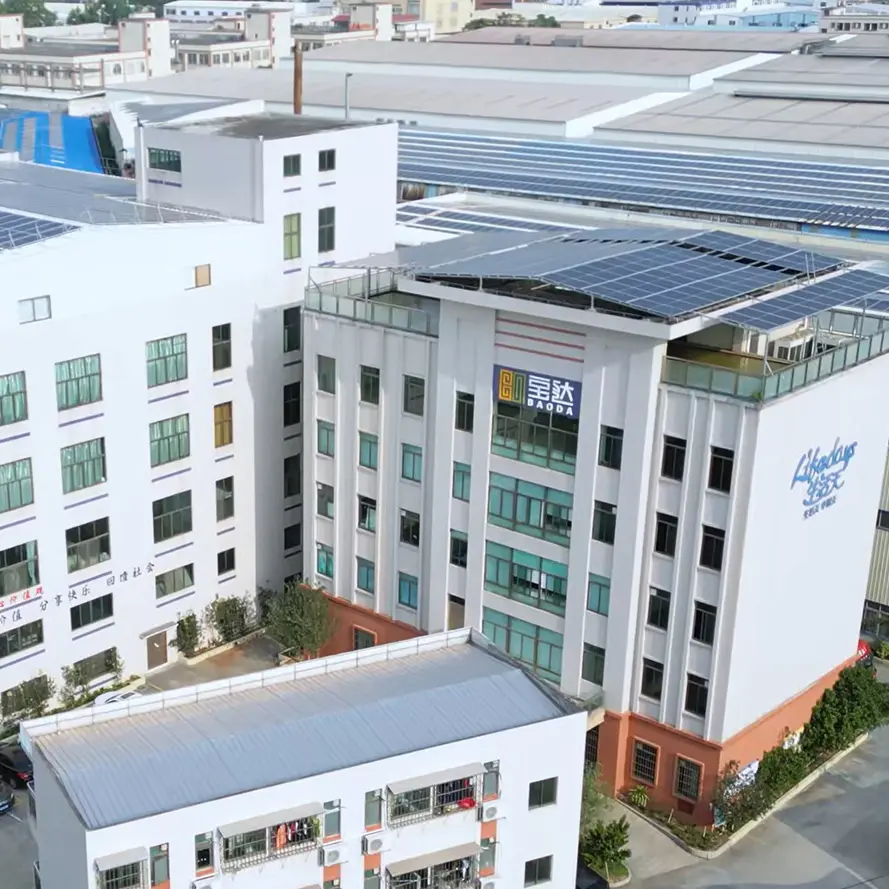
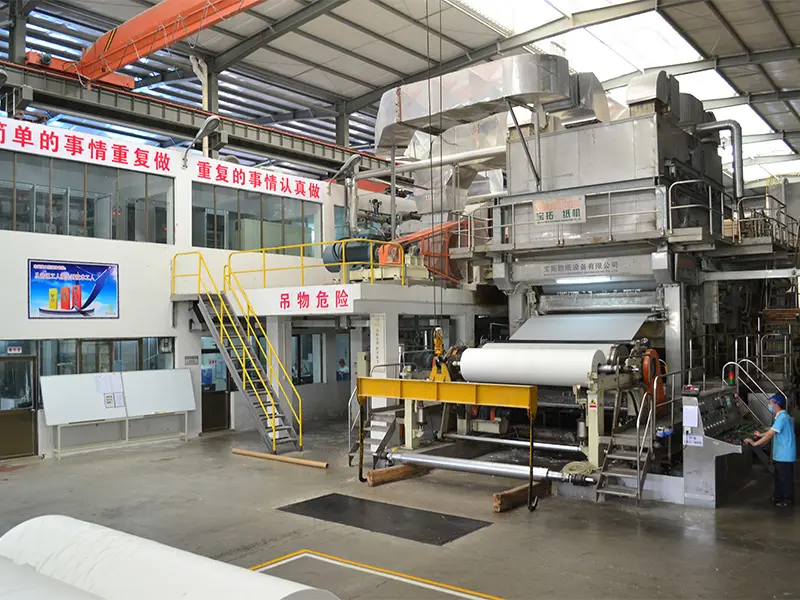
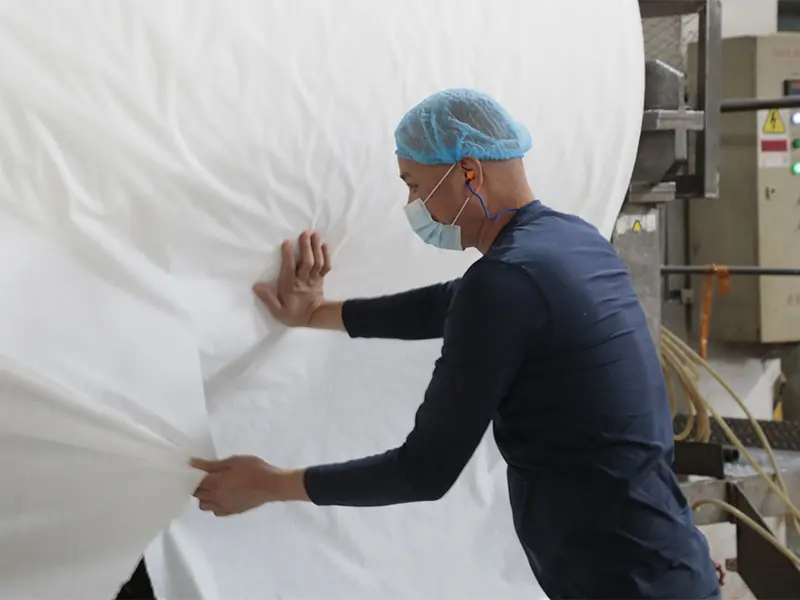
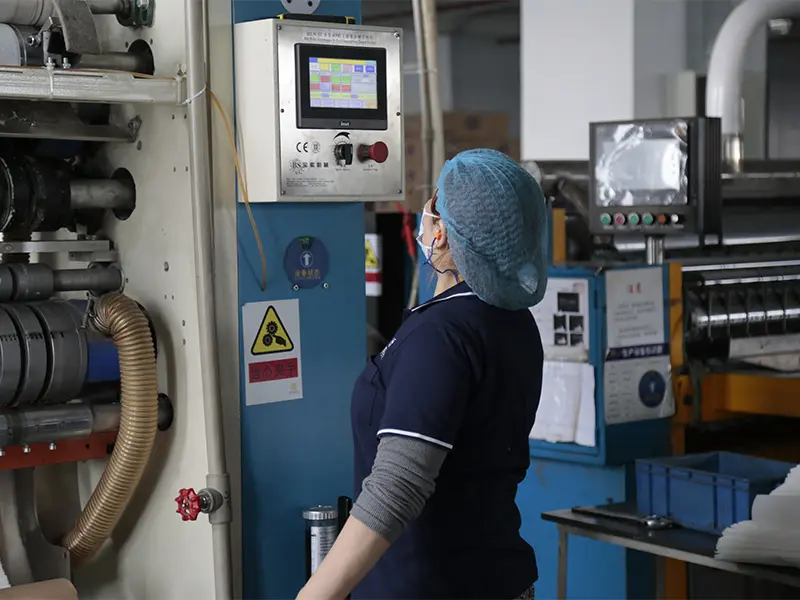
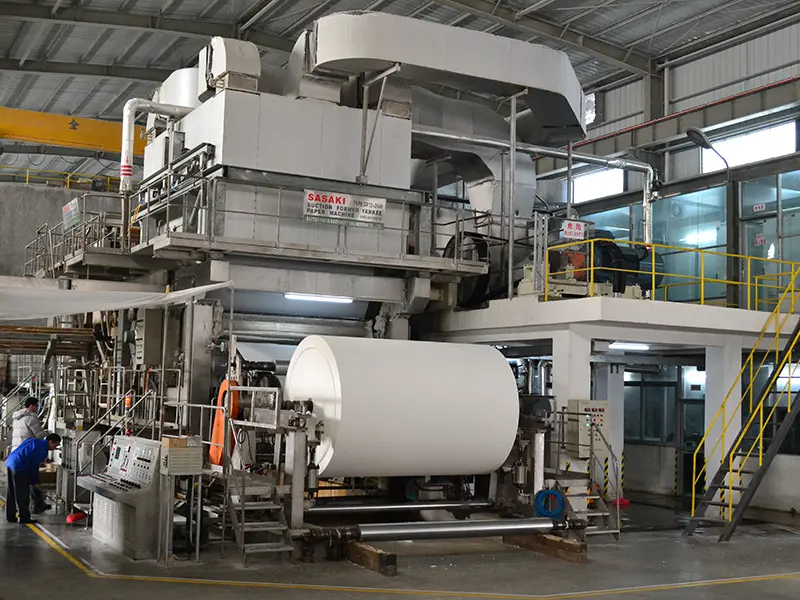
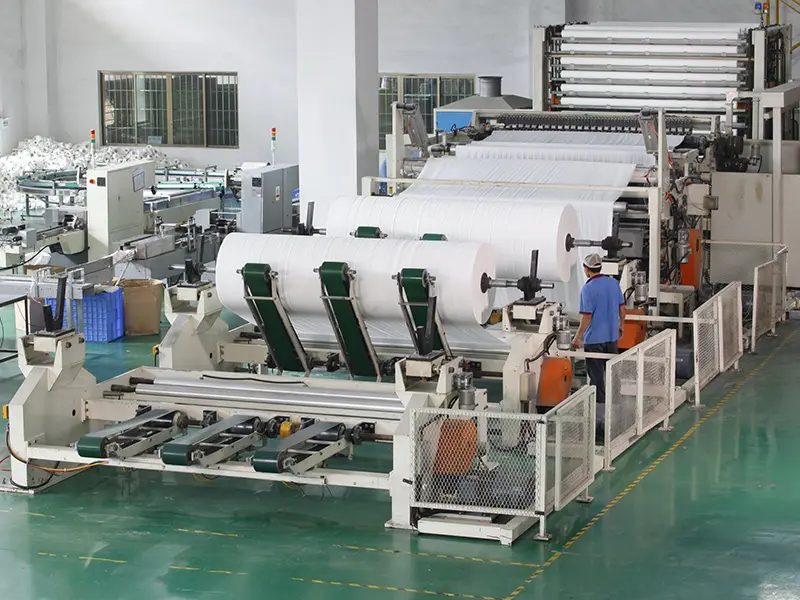
For over 27 remarkable years, since our inception in 1998, Baoda Paper Co., Ltd. has stood as an unwavering cornerstone of China's tissue paper industry, evolving from a domestic manufacturer into a globally recognized force. We have meticulously built our legacy on a formidable foundation of advanced manufacturing excellence and an unwavering commitment to quality. Our modern, sprawling complex, exceeding 20,000 square meters, is a testament to this commitment. Within its walls, we house state-of-the-art, imported high-speed paper machines and sophisticated automated processing lines. This powerful infrastructure is the engine behind our impressive annual production capacity of over 30,000 tons, enabling us to meet large-scale demands without compromising on the consistent quality that defines the Baoda name.
By leveraging advanced raw pulp processing technologies and optimizing ply-bonding systems, we deliver products that excel in tensile index, water absorption capacity, and softness metrics. Our facility is engineered for energy-efficient production, reflecting the macro industry shift towards greener operations.
Our comprehensive and curated product portfolio is designed to provide complete one-stop solutions for diverse market needs. We offer an extensive range of products, from essential household items like premium toilet rolls, versatile kitchen towels, and soft facial tissues to convenient and hygienic pocket tissue packs for on-the-go use. Understanding the diverse paths to market success, our business model is both robust and flexible. While we proudly market three successful self-owned brands, we are also a premier partner for clients seeking to build their own product lines. We specialize in tailored ODM (Original Design Manufacturing), OEM (Original Equipment Manufacturing), and OBM (Original Brand Manufacturing) services, working collaboratively to bring our clients' unique visions and brand identities to life with precision and expertise.
As urban densities increase and hygiene expectations escalate post-pandemic, the macro requirements of toilet tissue and kitchen paper procurement are undergoing profound technological and ecological changes.
Global regulations and consumers alike demand strict adherence to environmental metrics. Products must be manufactured using 100% virgin wood pulp from responsibly managed forests (FSC certified) or recycled fibers. Reducing carbon footprint at every processing stage is no longer optional but a prerequisite for entering tier-1 retail channels in the US, Europe, and Australia.
Modern hygiene solutions require optimal structural integrity. The industry is shifting from conventional 1-ply systems to advanced 2-ply, 3-ply, and 4-ply structural configurations. By utilizing micro-embossing and glue lamination, manufacturers can build a network of air pockets that increase both bulk softness and wet tensile strength.
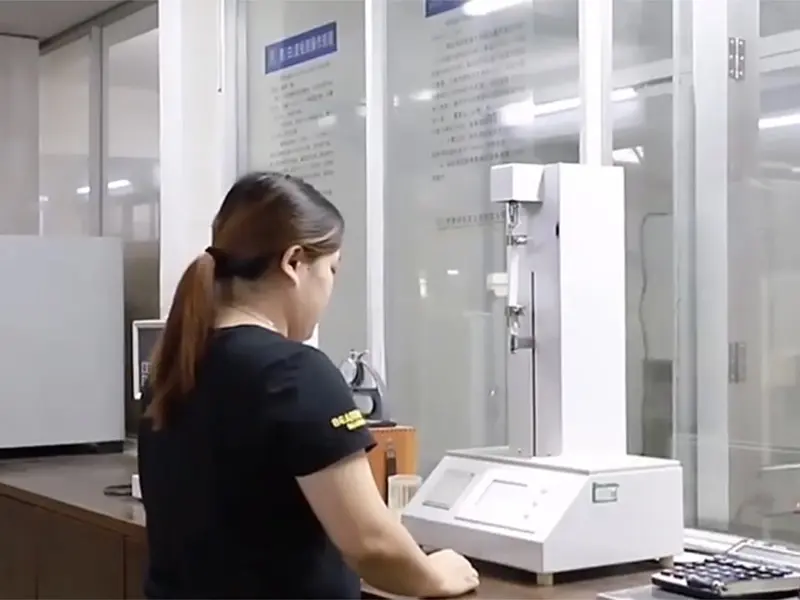
Advanced tissue mills now use high-speed automated winding, cutting, and wrapping lines. Incorporating real-time vision sensor systems allows automated detection of paper tearing, uneven basis weight, and perforation defects. This assures high-volume consistency for international OEM/ODM clients.
Enterprise-level buyers from supermarket chains, hotels, and health institutions look beyond unit price to assess the total cost of ownership and supplier capability.
For B2B buyers, sheet breakage on high-speed commercial dispensers leads to user dissatisfaction. Quality tissue rolls require optimization of the long-to-short fiber ratio during pulp preparation to ensure high cross-direction (CD) and machine-direction (MD) tensile strength.
Kitchen towels and industrial napkins must possess superior fluid retention. Through advanced glue-lamination and pocket embossing, the water-holding capacity is increased by up to 200%, translating into less tissue consumption per task and direct cost savings for end consumers.
Optimizing shipping container capacity is vital. Compressed packaging technology allows more rolls to be packed per cubic meter, lowering ocean freight expenses. At the same time, individual packaging must offer high moisture barriers to safeguard product integrity during transit.
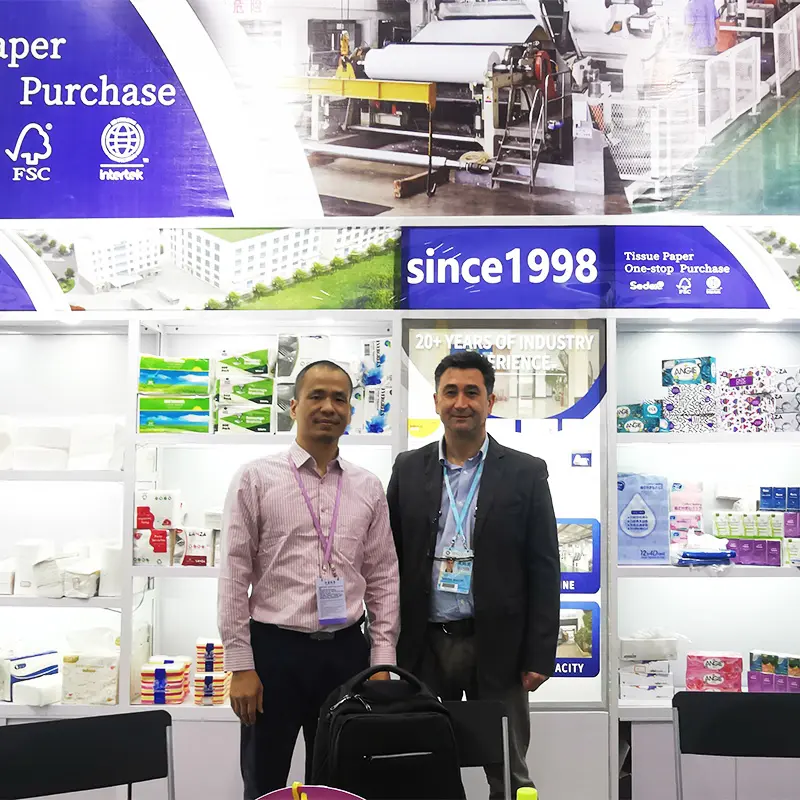
Our commitment to rigorous B2B solutions has earned us the trust of a vast network of over 10,000 global leaders in retail and distribution, including renowned giants such as Walmart and Watsons. By maintaining high-standard quality control processes throughout our operations, we guarantee that every shipment adheres to strict international expectations.
From pulp selection to customized embossing, our flexible production lines accommodate high-volume bespoke requirements.
We configure sheet dimensions, ply counts (1-ply up to 4-ply), and roll weights to match the local purchasing patterns of your target market. All parameters are meticulously documented to ensure identical batch reproduction.
Choose from an array of embossing patterns (edge-embossed, micro-embossed, or fully-laminated patterns) that enhance handfeel. Our engineering team assists in developing eye-catching graphics for outer wraps and carton display boxes.
For distributors looking to deploy their own brands, we provide comprehensive product lifecycle support, consistent raw material supply contracts, and predictable lead times to maintain market momentum.
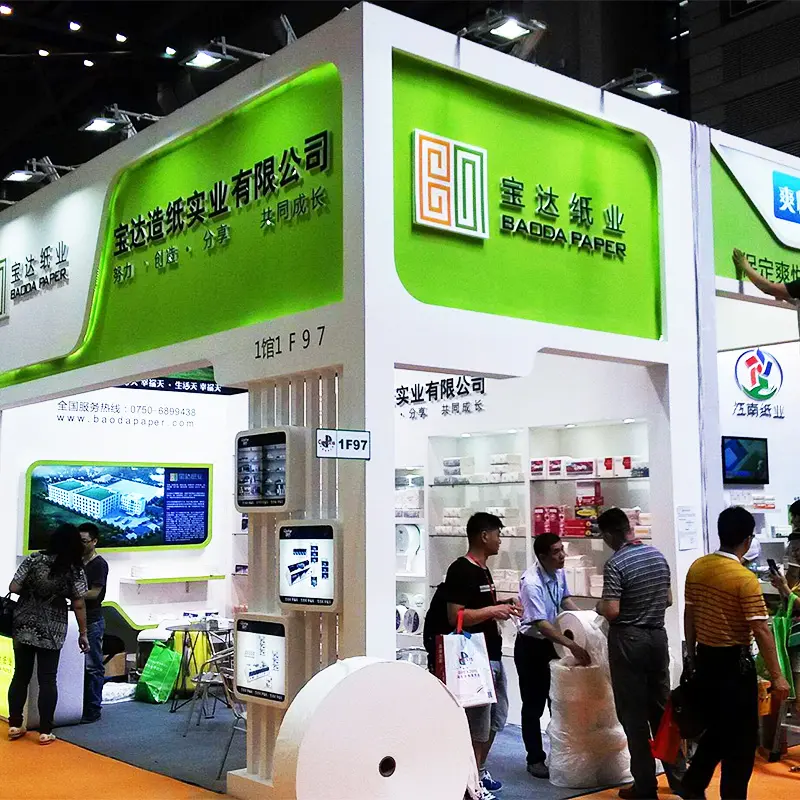
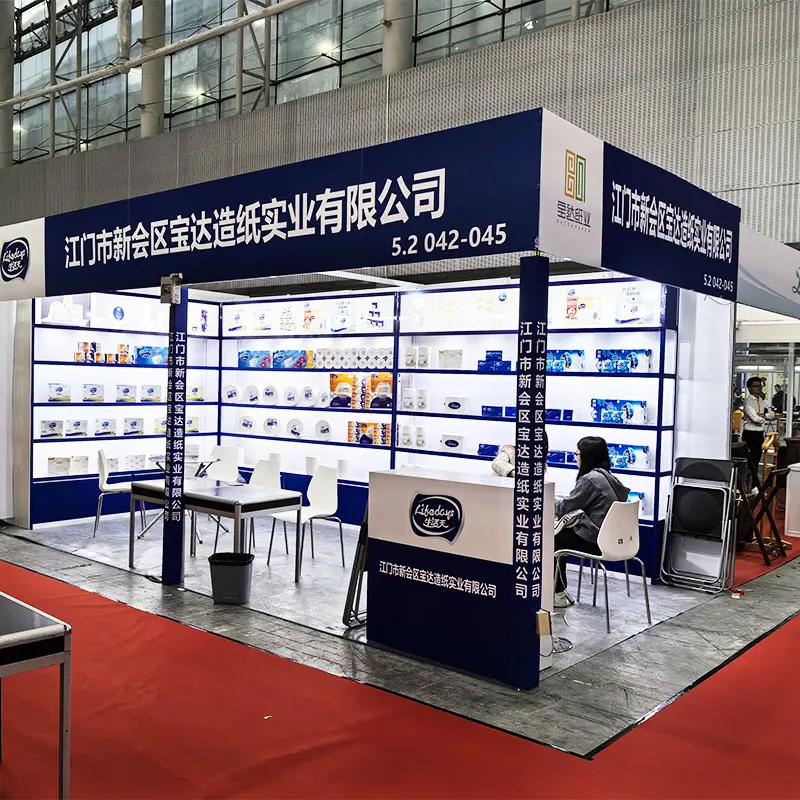
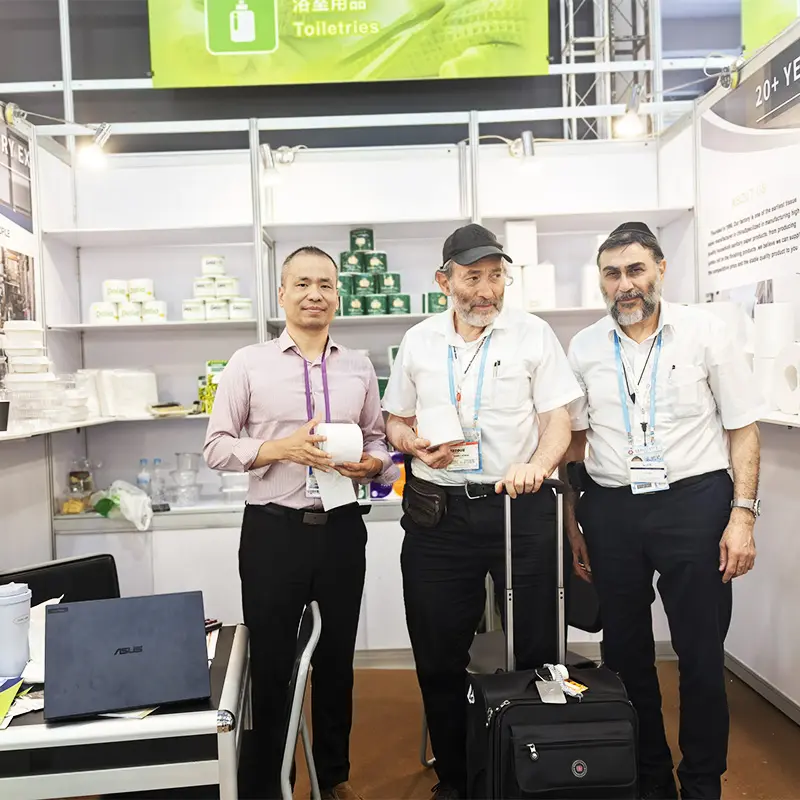
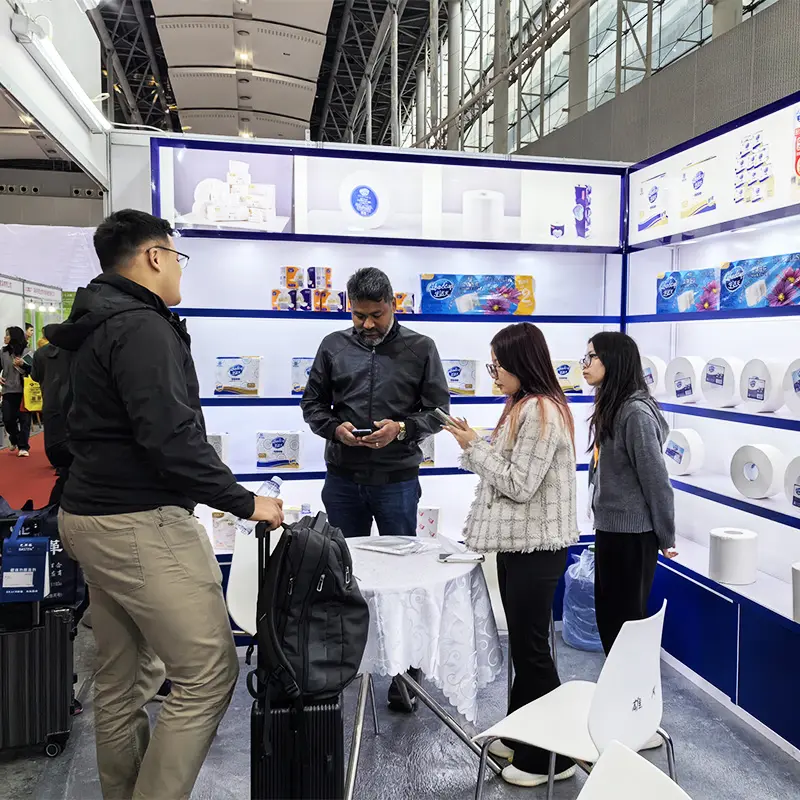
We maintain a rigorous quality assurance framework to ensure full regulatory compatibility in every international market.
Exporting to premium markets such as the USA, Australia, and Western Europe requires compliance with stringent chemical safety standards. Our products undergo rigorous lab evaluations to guarantee they are free from harmful chlorine brighteners, heavy metals, and optical fluorescent agents.
Moreover, our operations adhere strictly to local custom regulations, simplifying international B2B port inspections. We handle all complex export documentations, Certificate of Origin filings, and bills of lading to guarantee stress-free delivery.
Our commitment is backed by international certifications that validate our management and production consistency. These milestones represent our continuous investment in facility upgrades and eco-management.
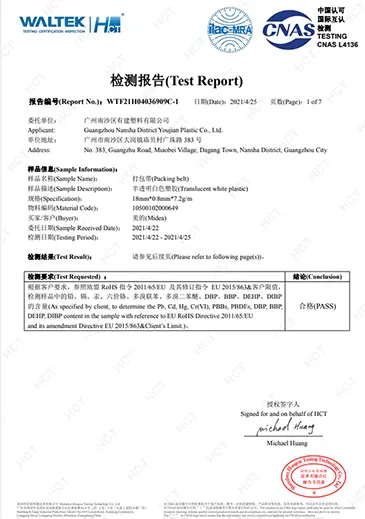
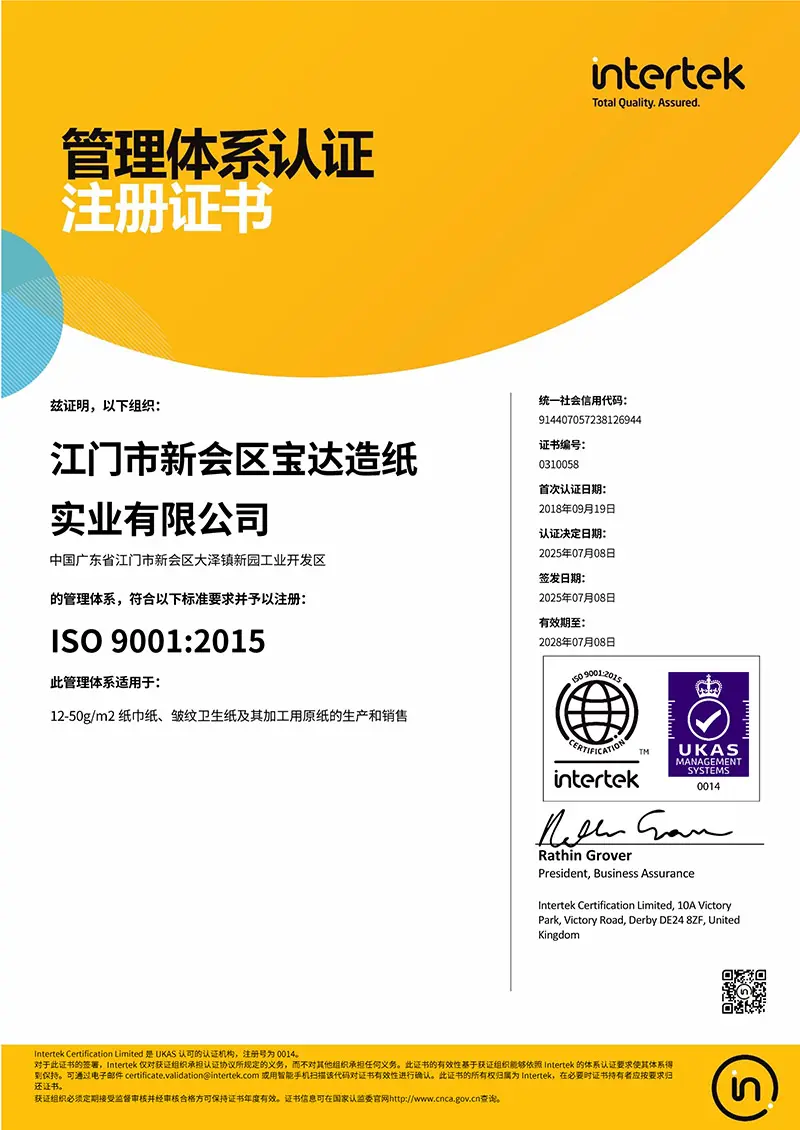
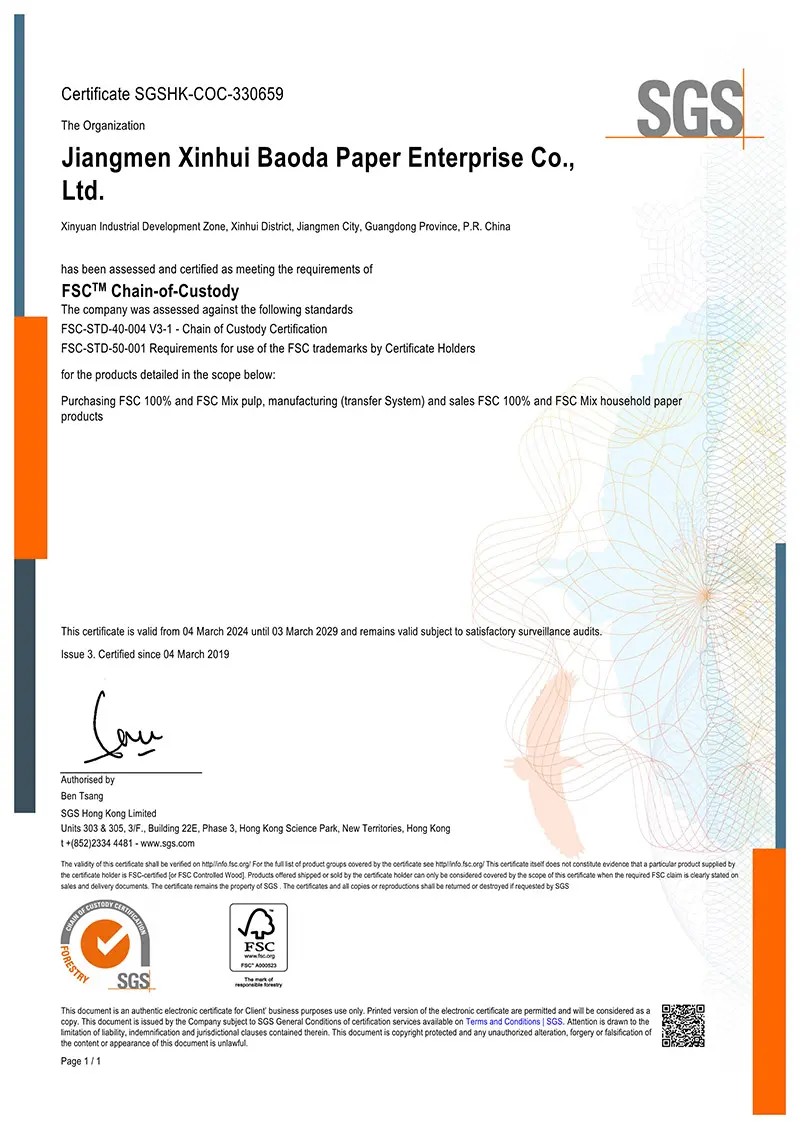
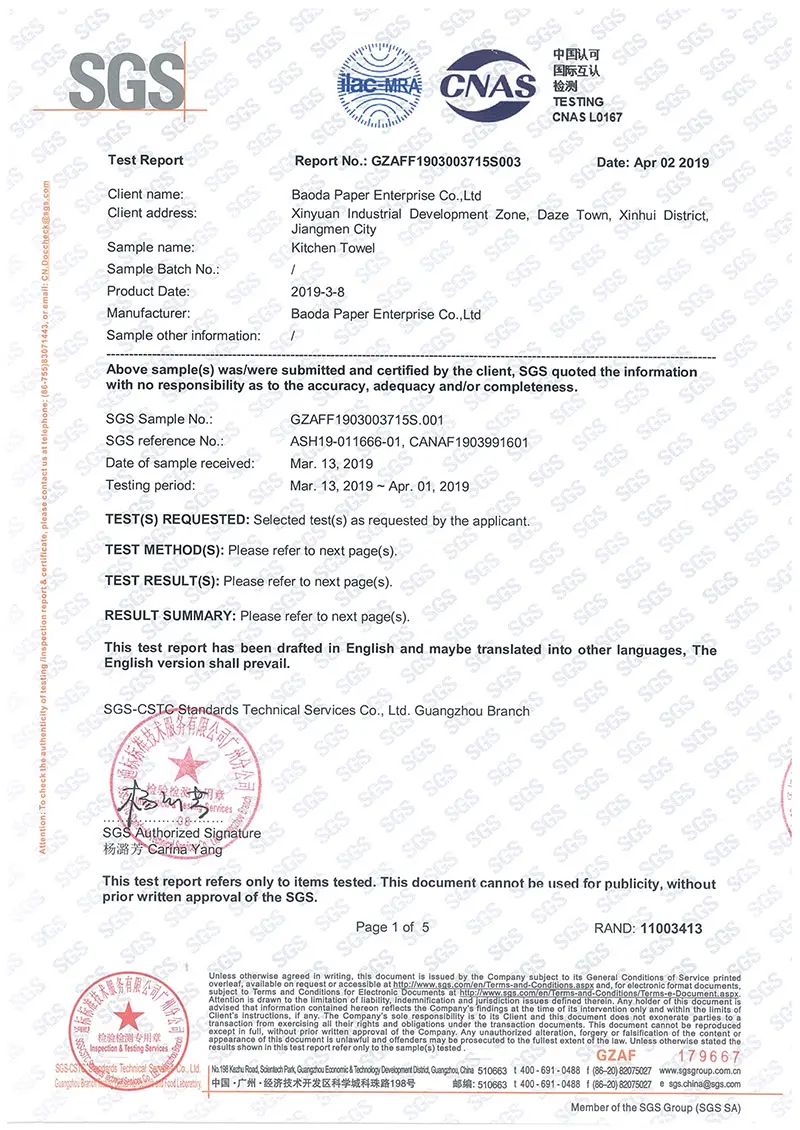
Investing in advanced technologies to continuously optimize paper bulkiness, softness, and absorption performance.
By shifting to TAD processing in upcoming line expansions, we aim to double the bulkiness of our high-ply tissues. TAD technology uses warm air to dry the paper web while it is on a structured screen, rather than pressing it against a hot cylinder. This process preserves the fiber structure, achieving superior softness without sacrificing tensile strength.
Responding to international plastic bans, our packaging research division is finalizing water-resistant paper wraps for individual toilet rolls and kitchen towels. These materials are 100% biodegradable and compostable, facilitating zero-waste distribution for environmentally conscious retailers.
To diversify raw material dependencies, we are expanding our bamboo pulp and wheat straw fiber integration lines. Bamboo fiber, with its unique long-fiber characteristics and natural antimicrobial properties, provides an exceptionally strong structural network ideal for heavy-duty kitchen towels and industrial wipers.
Answers to critical questions concerning logistics, customization, raw material sourcing, and compliance.
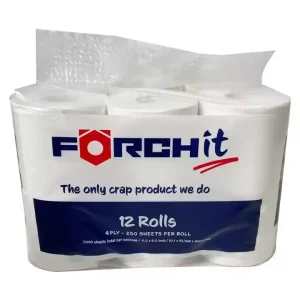
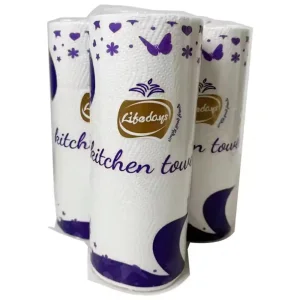
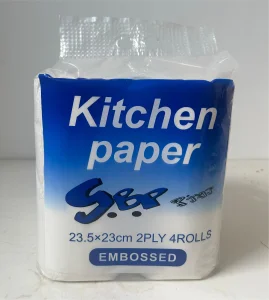
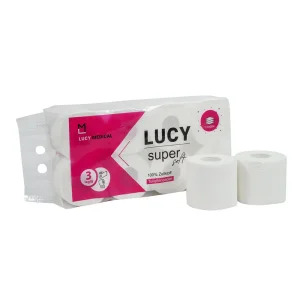
Premium white toilet tissue, glue-laminated kitchen towels, and customized restaurant napkins.
 BAODA PAPER